Blank & datum preparation
Turning establishes the bore, faces, shoulders and reference diameters used by later gear and spline operations.
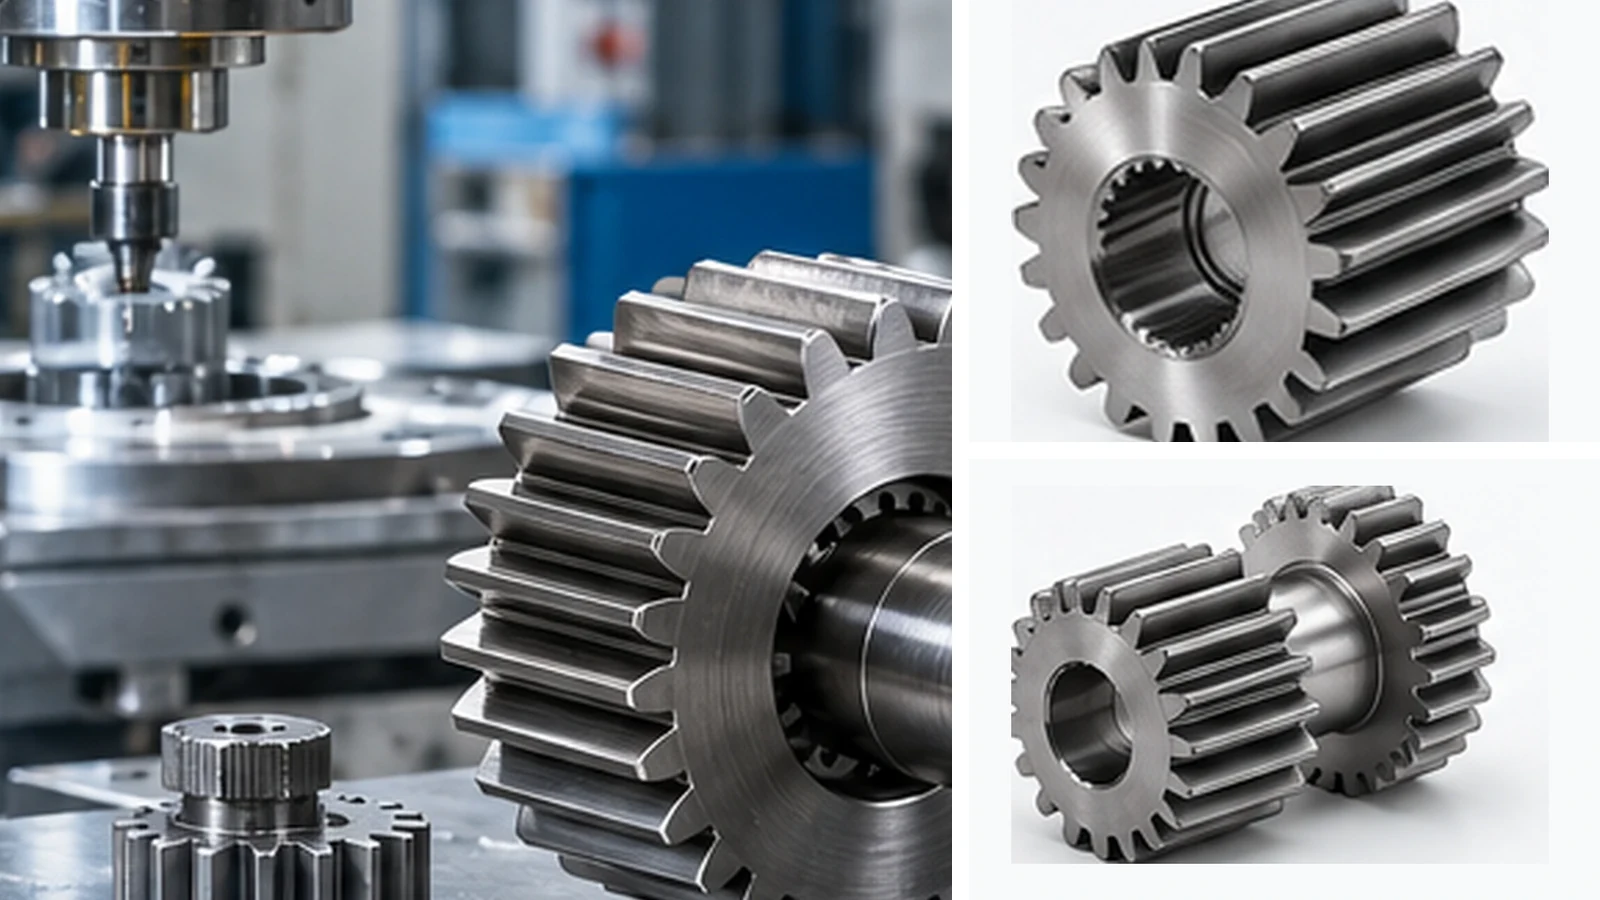
The manufacturing route follows the drawing: blank preparation and turning, tooth generation, heat treatment, optional finishing, spline/shaft machining and inspection as required.
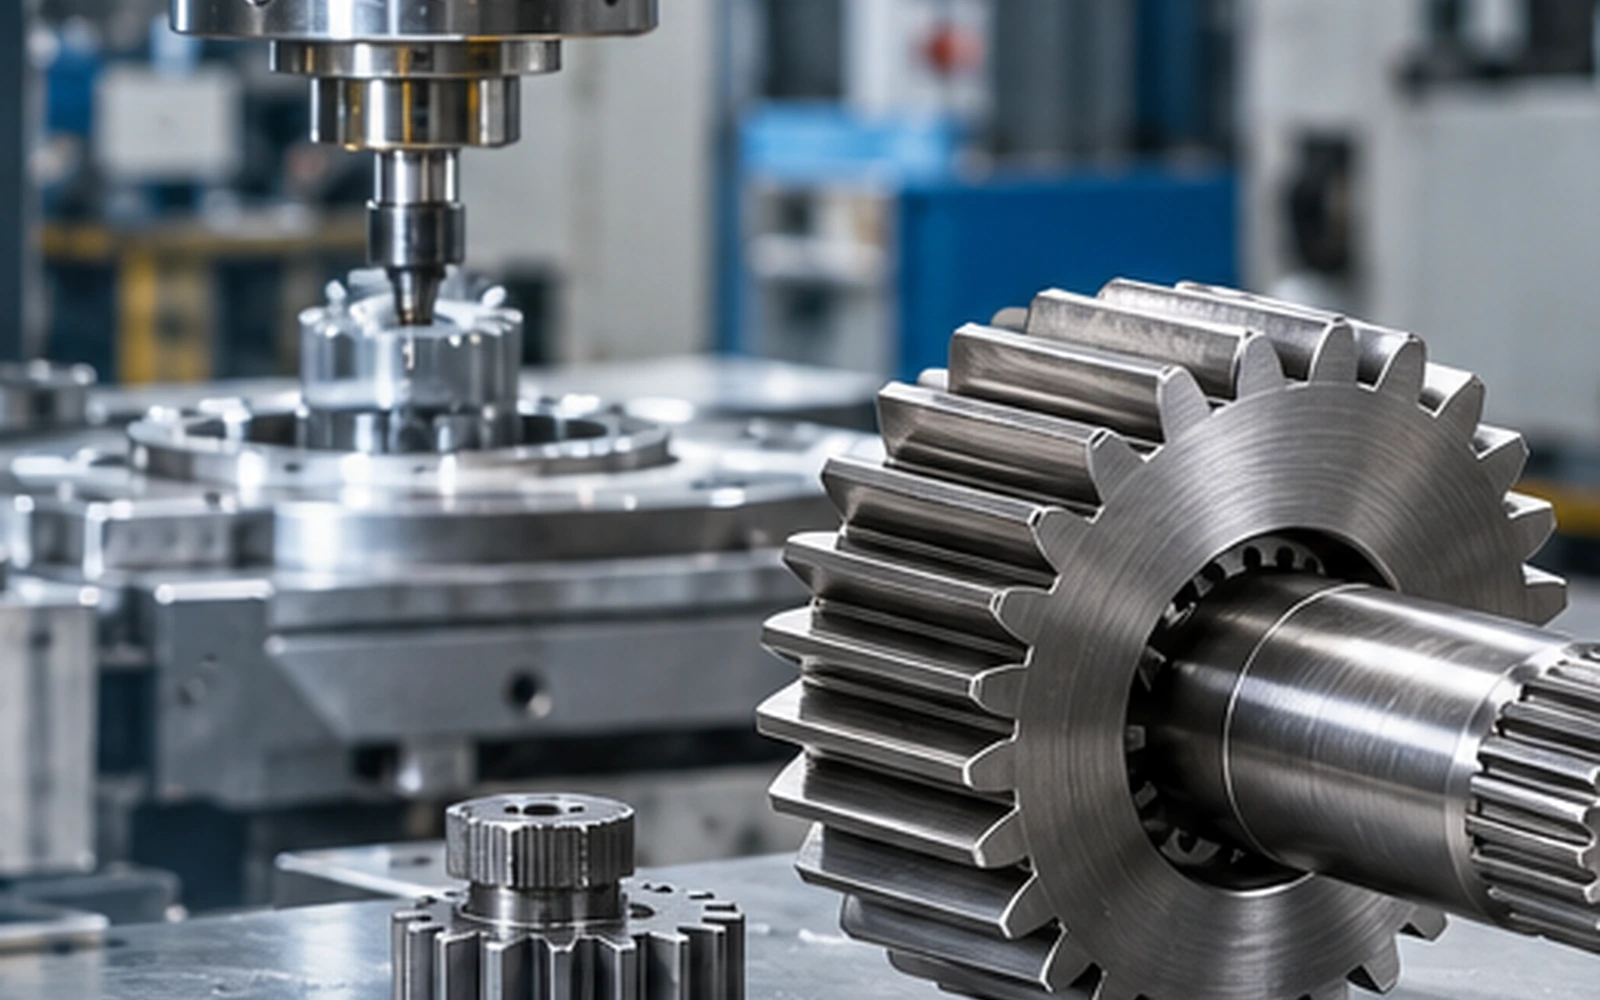
Not every sun gear needs every operation. The process should be selected from the drawing and duty.
Turning establishes the bore, faces, shoulders and reference diameters used by later gear and spline operations.
Hobbing or shaping can be used for external tooth generation depending on geometry, access and required process.
Internal or external spline, shaft journals, threads, keyways and retention features are machined to the controlled drawing.
Material and hardness requirements are applied according to the drawing and application duty; case requirements should be stated explicitly.
Grinding or other finishing is used when the drawing requires tighter tooth quality, runout or surface-finish control.
Inspection can include tooth thickness/span/over-pin measurements, runout, profile/lead data and interface dimensions as specified.
A dimensional report is useful only when it covers the characteristics that control assembly and mesh. For replacement gears, bore or spline fit, tooth thickness, runout and mating geometry usually deserve more attention than cosmetic measurements.
Tell us which records must accompany the shipment so the inspection plan is agreed before production.
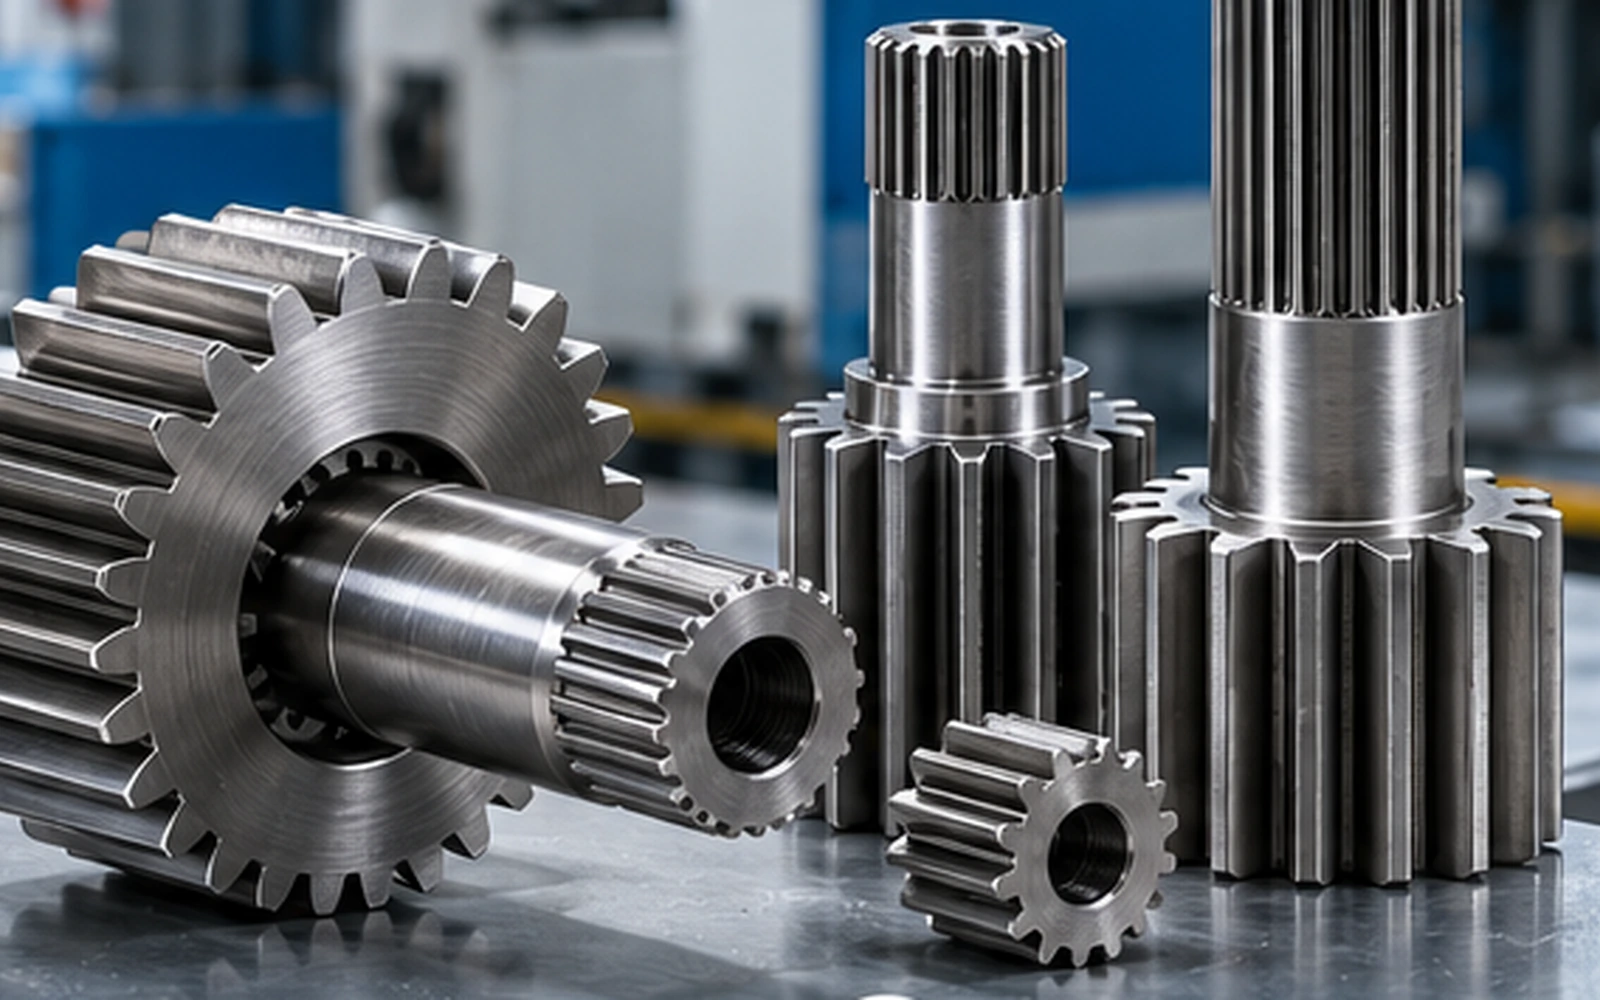
Machine the reference surfaces that will control later tooth and interface operations.
Generate external teeth and machine bore, spline or shaft features to the planned datum scheme.
Apply the controlled hardness/case route with allowance for distortion and final finishing.
Finish critical teeth or bearing/interface surfaces and verify the characteristics required by the drawing.
| Topic | Buyer guidance |
|---|---|
| Inspection is selective | Measure the characteristics that protect function rather than adding generic paperwork. |
| Heat-treatment effects | Plan stock and datum recovery before hardening when post-treatment finishing is required. |
| Integrated shaft risk | Long shaft parts can need extra straightness/coaxiality attention after treatment. |
| Packaging is part of quality | Protect finished teeth, splines and bearing seats from corrosion and metal-to-metal contact. |
Veuillez nous envoyer le dessin, les données de denture, les informations sur les composants d'accouplement, le droit de passage et la quantité. Nous examinerons l'interface avant de vous établir un devis.